UHMW-PE vs HDPE: Key Differences for Wear Parts – Which One Should You Choose?
Quick answer
UHMW-PE wins most abrasive wear, impact, and sliding-life jobs. HDPE wins when you need easier machining, lower cost, large welded structures, or moderate wear only. Similar density does not mean similar service life.
UHMW-PE and HDPE are both polyethylene—so buyers often treat them as interchangeable plate. On wear strips, chain guides, and impact pads, that shortcut creates early failures. Molecular weight (and thus abrasion resistance and toughness) is the real separator.
Material Overview
HDPE
High-density polyethylene is stiff relative to LDPE, chemically resistant, weldable, and economical. It machines more predictably than UHMW for many geometries, but its wear life under sliding abrasion is limited compared with UHMW.
UHMW-PE
Ultra-high molecular weight PE has extremely long chains that deliver outstanding abrasion resistance and impact toughness, with a low friction surface. It is harder to machine cleanly (stringy chips, stress relief quirks) and usually costs more per blank.
Density values sit near each other—see the plastic density chart—so weight alone will not decide this RFQ.
Key Differences for Wear Parts
| Factor | UHMW-PE | HDPE |
|---|---|---|
| Abrasion / sliding wear | Excellent | Moderate |
| Impact toughness | Outstanding | Good |
| Coefficient of friction | Very low | Low |
| Machinability | Trickier (gummy/stringy) | Easier |
| Welding / sheet fab | Limited vs HDPE | Common (tanks, liners) |
| Cost | Higher | Lower |
| Typical wear parts | Guides, wear strips, star wheels | Guards, spacers, mild guides |
Application Picks
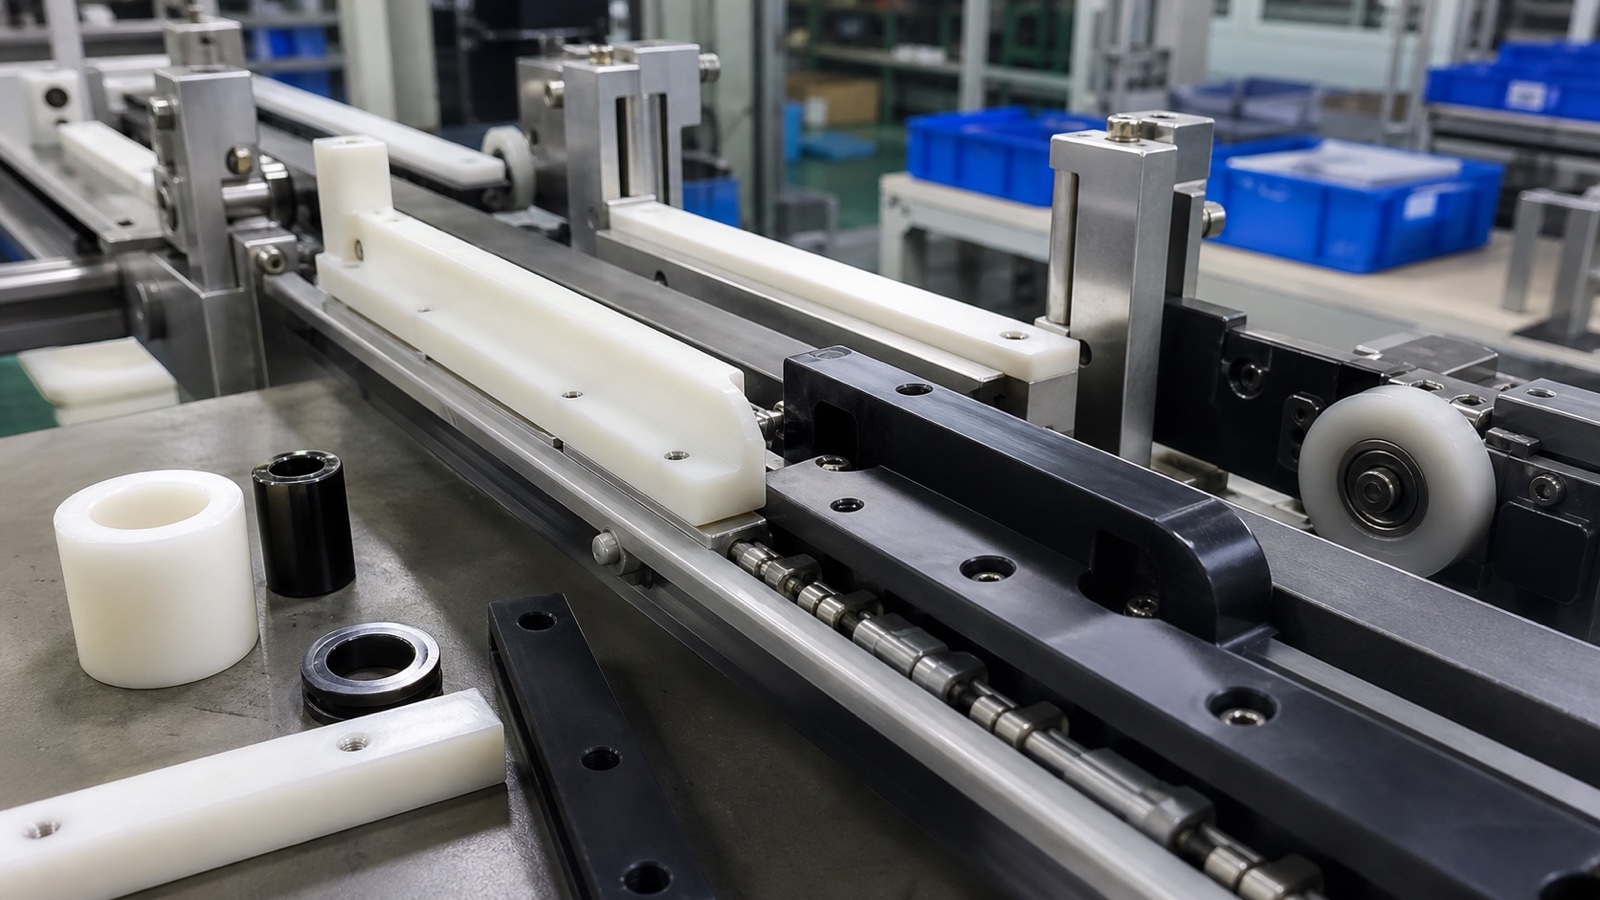
- Specify UHMW-PE: conveyor wear strips, chain guides, hopper liners with abrasive product, dock fenders, high-cycle star wheels
- Specify HDPE: tanks, cutting boards (grade-dependent), low-duty spacers, cost-sensitive guards, welded assemblies
- Compare further: when acetal enters the wear conversation, revisit POM vs nylon for precision sliding fits UHMW cannot hold as tightly
Shop tip: If the part is a long, thin wear strip, UHMW can move after machining. Machine with sharp tools, support the cut, and avoid overheating—then verify flatness before ship.
Machining, Cost, and Practical Quoting
UHMW wants very sharp cutters, intentional chip load, and patience on surface finish. HDPE still needs heat control (see the melting point chart) but is generally faster to program and finish. Quote UHMW with extra handling time when tolerances are cosmetic-critical.
Thickness and Design Notes
UHMW wear strips often need enough thickness to absorb abrasive embedding and to allow re-machining or flip-over life. HDPE covers and guards can run thinner when loads are low. Avoid over-constraining UHMW in a metal sandwich that does not allow thermal expansion—polyethylene expands more than steel.
Mating surfaces
UHMW sliding on polished stainless often works well dry. Aggressive grit, hot fines, or mismatched PV (pressure × velocity) still wear any PE. If temperatures approach the melting region, revisit the melting chart and consider a higher-temp wear material.
Frequently Asked Questions
Can HDPE replace UHMW to save money?
Only on mild duty. If abrasive wear is the primary load, HDPE usually loses life and creates more downtime than it saves.
Is UHMW always slippery enough to skip lubrication?
Often yes in dry sliding against many counterparts, but verify PV limits and mating surface. Design beats assumptions.
Do they machine with the same feeds?
No. UHMW is more forgiving of impact but less forgiving of dull tools and poor evacuation. Treat them as different processes.
Conclusion
Choose UHMW-PE when wear life and impact dominate; choose HDPE when cost, weldability, and moderate duty dominate. If you share abrasion media, speed, and load, PlasticCNCPro can recommend thickness, grade, and a machining approach that matches the conveyor—not just the catalog name.
RFQ Support
Send Your Drawing for a Quote
Share your 2D drawing, 3D model, material, quantity, tolerance, surface finish, and application details. Our team will review manufacturability and reply with a practical quotation.
Email: info@plasticcncpro.com
Address: 29 Fuxing Road, Dongguan City, Guangdong Province, China