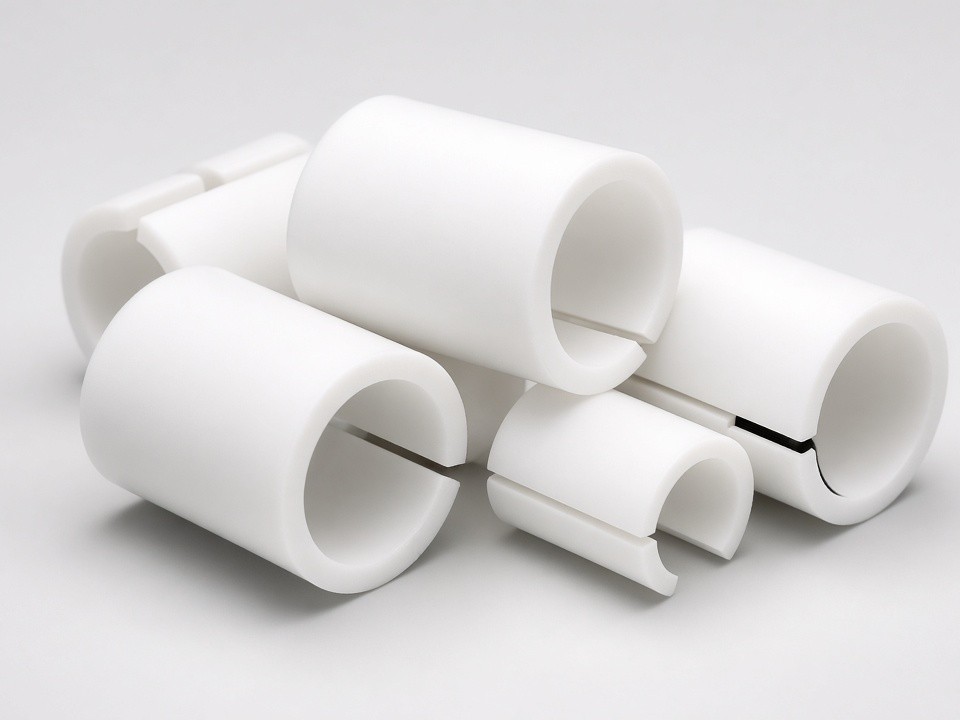
Custom Plastic Split Bushings
CNC-milled and turned split bushings for industrial equipment, automation systems, pumps, valves and machinery where full-circle bushings cannot be installed.
±0.05 mm
Standard OD and ID tolerance
1–50 pcs
Prototype quantities
2 days
Quotation review target
Built for service-critical assemblies
Install around shafts or rods without disassembly.
Design fundamentals
A split feature engineered for alignment and movement
01
Accessible installation
Install around shafts or rods without removing the surrounding assembly.
02
Stable slot geometry
The longitudinal cut maintains alignment under load while controlling slot width and parallelism.
03
Thermal freedom
Material and slot design help accommodate thermal expansion and prevent binding.
Material engineering
Polymer options matched to your operating envelope
We review operating temperature, chemical contact, PV value, moisture exposure and required service life before recommending a material.
General wear
POM / Acetal for dependable wear performance and dimensional control.
Moderate loads
Nylon 6 and 66 for applications requiring practical strength and wear resistance.
Impact and sliding
UHMW-PE for demanding sliding contact and impact conditions.
Chemical exposure
PTFE and PVDF for chemically challenging environments.
Elevated temperatures
PEEK and PPS for high-temperature service requirements.
High-pressure zones
PAI for applications demanding high-pressure performance.
Filled grades when the specification demands more
Glass, carbon fiber or PTFE additives are selected when friction control or dimensional stability exceeds the capability of unfilled grades.
CNC process
From stock material to inspection-ready component
Split bushings start from bar or plate stock. Turning and milling operations are sequenced to maintain dimensional accuracy and keep secondary work efficient.
Send your drawing-
Turn the OD and bore
Outer diameter and bore are machined to final dimensions from bar or plate stock.
-
Mill the split slot
Precision cutters control slot width and parallelism for consistent installation and service.
-
Add integrated features
Threaded holes, keyways and retaining grooves are added in the same setup when required.
-
Finish and verify
Deburring, chamfering and surface finishing are followed by dimensional inspection and reporting.
Production confidence
Measured for fit, repeatability and scale
±0.025 mm
Tighter tolerance available
Standard OD and ID tolerance is ±0.05 mm, with ±0.025 mm available on request.
±0.1 mm
Controlled split width
Slot width is controlled to ±0.1 mm or tighter according to drawing requirements.
Inspection documentation available
Every batch receives first-article inspection with CMM or digital micrometers. Material certificates and dimensional reports are supplied when requested.
Built for your production stage
Low-volume flexibility without a tooling barrier
Prototype quantities from one to fifty pieces are run on the same machines used for repeat orders of several hundred units. No molds are required, keeping tooling costs low while your design moves through fit and function testing.
Validate the fit
Order initial samples for installation, clearance and function testing.
Refine the specification
Review material, tolerance and wear performance before production release.
Scale with confidence
Continue with repeat orders of several hundred units using the same CNC process.
Application range
Designed around real equipment constraints
Split bushings are selected when shaft removal is impractical or thermal cycling could cause seizure in a solid bushing.
Technical questions
What to confirm before production
Request a quotation
Turn your split bushing design into a production-ready part
Share your drawing or model, material preference, quantity, tolerance notes and application details. We will confirm manufacturability and respond with pricing within two working days.
Quotation contact: info@plasticcncpro.com
Sample shipment address: 29 Fuxing Road, Dongguan City, Guangdong Province, China