
Engineering materials guide
PAI vs. PEI Density: Weight and Performance Comparison Guide
We compare PAI and PEI density, component weight, strength, heat resistance, wear behavior, chemical stability, machinability, and total value so engineers can select the right high-performance thermoplastic for demanding applications.
Introduction
PAI, or polyamide-imide, and PEI, or polyetherimide, are elite engineering thermoplastics used where ordinary plastics cannot provide enough heat resistance, dimensional stability, strength, or chemical durability. Both are amorphous, high-performance polymers, but they are not interchangeable in every design.
For aerospace, automotive, semiconductor, medical, fluid-handling, and industrial equipment designers, density is more than a material-table number. A difference of roughly 0.1 to 0.2 g/cm³ affects the weight of every machined or molded component. That change must then be considered alongside strength, stiffness, temperature, friction, moisture, tolerances, and manufacturing cost.
The practical question is not simply “Which polymer is stronger?” It is “Which material delivers the required performance with acceptable mass, manufacturability, service life, and total cost?”
In this guide, we explain the PAI density versus PEI density difference and connect it to real engineering decisions. At PlasticCNCPro, we use this same application-first approach when reviewing drawings, samples, tolerances, and material requirements for custom plastic parts.
Understanding Material Density: PAI vs. PEI
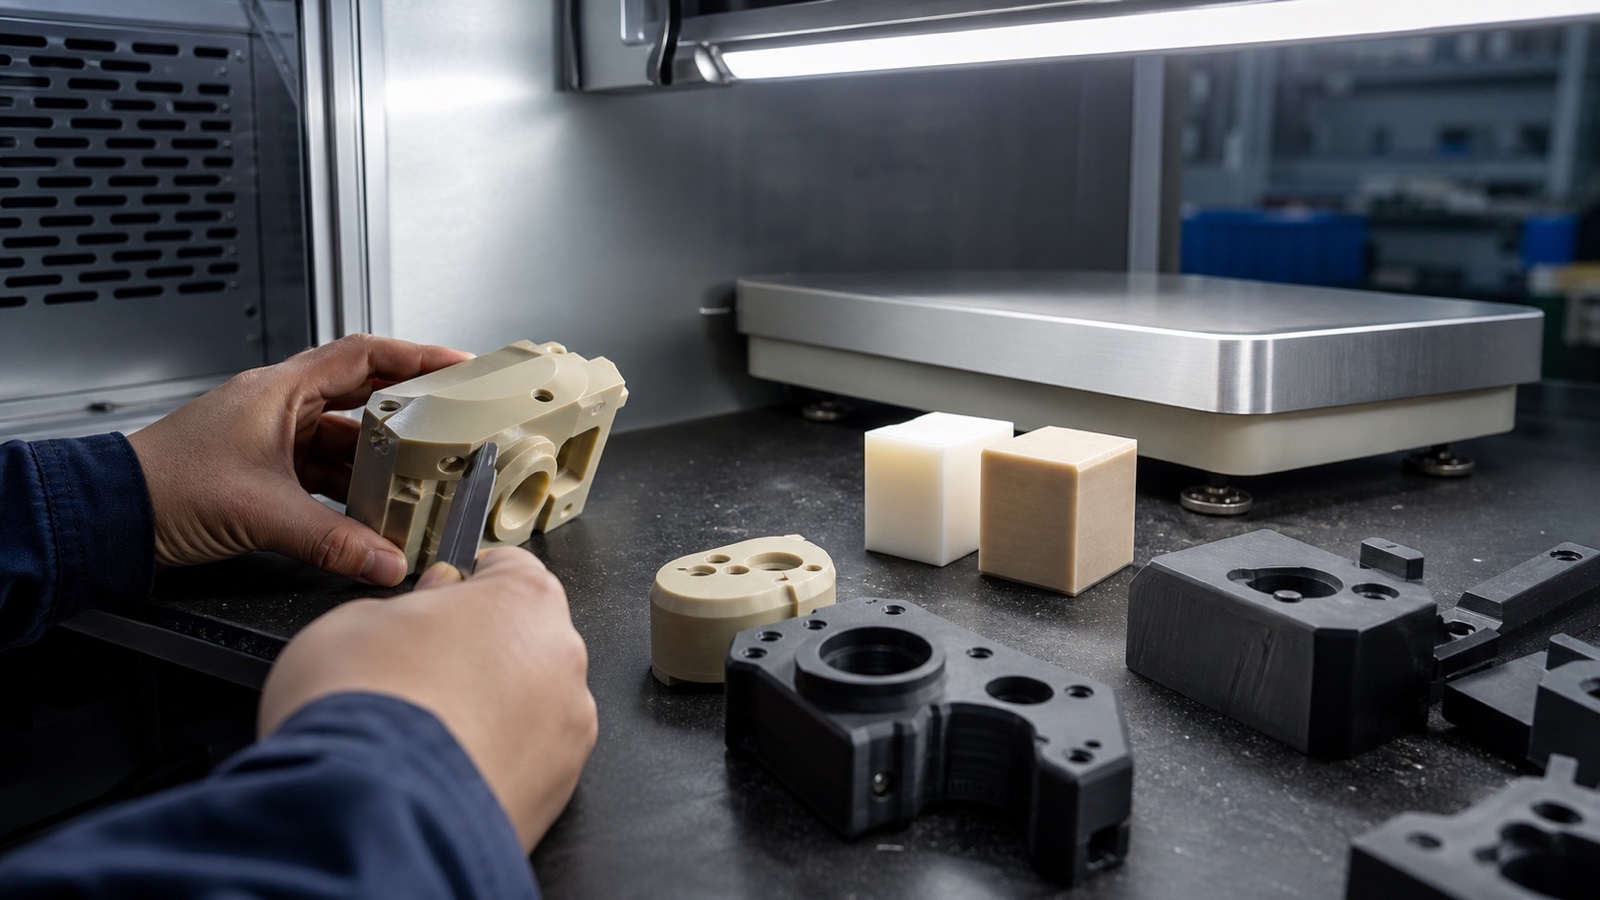
Density is mass per unit volume. For a component with the same geometry, a higher-density polymer produces a heavier part. Typical published values for neat, unfilled grades are approximately 1.40–1.45 g/cm³ for PAI and 1.27–1.30 g/cm³ for PEI.
| Material condition | Typical density | Approximate density in kg/m³ | Weight implication |
|---|---|---|---|
| Neat PAI | 1.40–1.45 g/cm³ | 1,400–1,450 kg/m³ | Higher mass for identical geometry |
| Neat PEI | 1.27–1.30 g/cm³ | 1,270–1,300 kg/m³ | Lower mass for identical geometry |
| Filled PAI or PEI | Grade-dependent | Grade-dependent | Reinforcement can increase density significantly |
How density changes component weight
For a 100 cm³ component, neat PAI would typically weigh about 140–145 g, while neat PEI would weigh about 127–130 g. The difference is approximately 10–18 g for this small volume. In a large assembly, or where many brackets, insulators, guides, bushings, or covers are used, that difference can become meaningful.
However, lower density does not automatically mean lower system weight. If PEI requires thicker walls, additional ribs, or a larger cross-section to meet the same load requirement, the finished PEI component may not be lighter than a smaller PAI component. We therefore compare density with allowable stress, stiffness, geometry, and safety factor rather than evaluating density alone.
Neat versus filled grades
A “neat” grade is the base polymer without reinforcing fibers or major functional fillers. Glass fiber and carbon fiber reinforced grades generally have higher density than the unfilled resin. They can also provide higher modulus, improved dimensional stability, reduced thermal expansion, or improved wear performance.
Glass-filled grades
Glass reinforcement can increase stiffness and dimensional stability, but it also changes density, anisotropy, surface finish, and machining behavior. Fiber orientation may matter in molded parts.
Carbon-filled grades
Carbon reinforcement can improve stiffness, thermal behavior, and sometimes wear performance. It may also affect electrical properties and tool wear, so the exact grade must be confirmed before production.
Design check
Always place the exact resin grade on the drawing or purchase specification. “PAI” and “PEI” identify polymer families, not one universal density or performance value.
Mechanical Strength and Stiffness Comparison
PAI is generally selected when the design priority is maximum strength, stiffness, compressive capability, and resistance to deformation under demanding loads. Its high mechanical performance makes it suitable for structural parts, precision wear components, and load-bearing elements that must retain geometry over time.
PEI provides a strong strength-to-weight balance and is often easier to justify when the part needs high general engineering performance without the full capability or cost of PAI. It offers good rigidity, useful toughness, and high impact resistance for many industrial and equipment applications.
| Design consideration | PAI tendency | PEI tendency |
|---|---|---|
| Load-bearing capacity | Usually the stronger choice for severe loads and sustained mechanical demand | Strong general-purpose performance for many engineered parts |
| Stiffness and modulus | Typically higher, especially in demanding structural applications | High stiffness with a lower density advantage |
| Impact behavior | Strong and durable, with grade and temperature effects to evaluate | Good balance of strength and impact resistance |
| Dimensional load retention | Excellent when temperature and load are especially severe | Very useful for stable industrial and equipment components |
For a structural bracket, clamp, support, or precision carrier, we would examine the actual force path, unsupported span, fastener loads, creep exposure, and operating temperature. A lower-density PEI design may be attractive, but PAI can allow a smaller section or provide a greater margin against deformation. The correct decision depends on the complete geometry and loading condition.
Thermal Performance and Heat Resistance
Thermal performance is one of the clearest differences between these polymer families. Both are designed for elevated-temperature service, but PAI generally maintains mechanical integrity at higher thermal extremes than PEI. This matters when a part is continuously loaded, exposed to repeated heat cycles, or located near a high-temperature process.
PAI thermal profile
Higher-temperature structural confidence
PAI is commonly chosen for applications where strength, stiffness, and wear resistance must remain dependable at severe temperatures. It is particularly attractive when thermal load and mechanical load occur together.
PEI thermal profile
High-temperature capability with lower material burden
PEI offers a high glass transition temperature and strong thermal stability for many industrial, electrical, medical, and transport applications. It is often sufficient where the thermal envelope is demanding but not at the upper limit of PAI capability.
Tg, continuous use temperature, and real service conditions
The glass transition temperature, or Tg, indicates the temperature region where an amorphous polymer changes from a relatively rigid glassy state toward a more rubber-like state. It is useful, but it is not a complete service-temperature rating. Continuous use temperature, sustained stress, cycle duration, atmosphere, and part geometry also affect performance.
A component can remain intact above its nominal Tg while losing stiffness or dimensional accuracy under load. For that reason, we recommend reviewing the material data sheet for the exact grade and comparing the temperature at which the part must carry its design load—not only the headline Tg value.
Thermal design rule
If heat is combined with pressure, sliding, vibration, or a tight dimensional tolerance, use the working temperature and load together when screening PAI and PEI.
Tribological Properties and Wear Resistance
Tribology concerns friction, lubrication, wear, and the interaction between moving surfaces. PAI is well known for strong wear resistance and useful self-lubricating behavior, especially in grades developed for bearing, seal, thrust washer, guide, and sliding applications.
This makes PAI a strong candidate for friction-heavy parts that must operate with limited lubrication, elevated temperatures, high contact pressure, or frequent movement. It can be used for precision bushings, wear rings, rollers, bearing retainers, and other components where replacing a worn part is difficult or expensive.
PEI can be sufficient where contact loads, sliding speed, temperature, and duty cycle are moderate. It may be a practical choice for guides, insulators, fixtures, housings, and low-to-moderate wear components, but it should not automatically replace a dedicated PAI wear grade in severe friction service.
| Application question | Preferred starting point | What to verify |
|---|---|---|
| Continuous sliding under load? | PAI, especially a suitable wear grade | Counterface, pressure, velocity, temperature, lubrication, and wear rate |
| Occasional movement or contact? | PEI may be sufficient | Impact, friction coefficient, surface finish, and duty cycle |
| Low-maintenance bearing or wear part? | PAI is often the safer screening choice | Exact grade data and application testing |
Chemical Resistance and Environmental Stability
PAI and PEI both offer strong resistance to many industrial environments, but “chemical resistant” does not mean resistant to every chemical at every temperature and stress level. Solvent concentration, exposure time, temperature, pressure, surface condition, and residual machining stress can change the result.
PEI is valued in electrical, laboratory, medical, automotive, and equipment applications where dimensional stability and resistance to many chemicals are required. PAI is also suitable for harsh service and can provide an advantage when chemical exposure is combined with heat, load, or wear.
Moisture, solvents, and long-term dimensional stability
Neither material should be approved from a generic compatibility chart alone. Moisture uptake, thermal cycling, cleaning agents, aggressive solvents, and sterilization or process conditions can affect dimensions and mechanical properties. For precision parts, we recommend checking both chemical compatibility and the dimensional change expected over the complete service life.
A practical environmental review
-
1
List every exposure
Include process fluids, cleaning chemicals, oils, fuels, gases, humidity, and occasional spills.
-
2
Add temperature and stress
Evaluate the chemical while the component is loaded and at its actual operating temperature.
-
3
Confirm with the grade supplier
Use grade-specific compatibility data or a representative immersion and stress test where failure is costly.
Machinability and Fabrication Considerations
Both PAI and PEI can be produced by injection molding or CNC machining, but the best process depends on volume, geometry, tolerance, tooling investment, and the need for design changes. CNC machining is often useful for prototypes, replacement parts, complex geometries, and low-volume production before committing to a mold.
PAI can be challenging to machine because of its hardness, strength, thermal sensitivity, and potential for dimensional movement if heat is not controlled. Tool selection, sharp cutting edges, stable workholding, appropriate feeds and speeds, and effective chip evacuation all matter. Filled grades may introduce additional tool-wear considerations.
PEI is generally easier to fabricate than PAI, although it still requires disciplined machining practice. Poor heat control, excessive clamping, or unsuitable tooling can create burrs, stress, dimensional drift, or a poor surface finish. We review thin walls, deep pockets, small holes, threads, and tolerance zones before quoting a custom part.
CNC machining note
For high-performance polymers, the material grade and machining strategy should be treated as one engineering decision. A strong resin can still fail to meet requirements if the process introduces stress or loss of dimensional accuracy.
Injection molding versus CNC machining
| Production situation | Often favorable process | Reason |
|---|---|---|
| Prototype or small batch | CNC machining | Avoids mold investment and allows rapid design iteration |
| Complex solid geometry | CNC machining may be practical | Suitable when the geometry is difficult or uneconomic to mold at low volume |
| Repeat high-volume production | Injection molding may become favorable | Tooling cost can be distributed across many consistent parts |
At PlasticCNCPro, we support CNC milling, turning, drilling, tapping, threading, slotting, and complex custom machining for PEI, PAI, and other engineering polymers. When reviewing a project, we consider not only whether a part can be made, but whether it can be made consistently at the required tolerance and surface quality.
Cost and Value Analysis: Why Are They Expensive?
PEI and PAI are expensive compared with commodity plastics because their raw material synthesis is more complex, their resin supply is specialized, and their manufacturing processes must achieve demanding thermal and mechanical performance. The price includes more than polymer volume; it reflects controlled production, specialized grades, processing requirements, and a smaller supply chain.
PAI may carry an additional premium where the grade provides exceptional strength, wear resistance, and high-temperature capability. PEI is also a premium polymer, but its lower density and broad performance balance can make it a more economical choice when the application does not need the full capability of PAI.
When does the performance premium make sense?
We recommend evaluating total cost rather than resin price alone. A more expensive polymer can be the lower-cost engineering solution if it extends service life, prevents frequent replacement, reduces lubrication, allows a smaller part, or avoids failure in a difficult-to-access machine.
Start with the failure risk
Identify whether the current concern is load, heat, wear, chemicals, moisture, dimensional drift, or electrical performance.
Compare the complete part cost
Include machining time, scrap risk, inspection, assembly changes, maintenance, downtime, and replacement frequency.
Select the least costly material that passes
If PEI meets the actual requirements, its lower density and balanced performance may offer better value than PAI.
Frequently Asked Questions
How strong is PEI plastic?
PEI is a high-strength engineering thermoplastic with a strong strength-to-weight ratio, good stiffness, and useful impact resistance. It is suitable for many structural, electrical, laboratory, medical, automotive, and industrial components. The exact strength depends on the grade, temperature, moisture exposure, geometry, and whether the material is reinforced.
What is the densest plastic?
There is no single answer without defining whether we mean neat polymers, filled compounds, or specialty materials. PAI and PEI are relatively dense compared with many common plastics, but their densities remain within the normal range for high-performance polymers. PTFE and heavily filled or mineral-reinforced polymers can be denser, while materials such as polypropylene and polyethylene are generally lighter.
Why is PEI plastic so expensive?
PEI requires specialized raw material synthesis, controlled production, and processing intended to deliver high thermal, mechanical, chemical, and dimensional performance. It also has a smaller supply chain than commodity plastics. For machined parts, the cost additionally reflects premium stock material, careful processing, inspection, and lower production volumes.
What is the density of PEI?
Standard neat PEI is typically around 1.27–1.30 g/cm³, equivalent to approximately 1,270–1,300 kg/m³. The actual value depends on the manufacturer and grade. Glass fiber, carbon fiber, mineral, antistatic, conductive, flame-retardant, and wear-modified grades can have different densities.
Conclusion: Choosing the Right Material for Your Application
PAI and PEI are both high-performance materials, but they serve different optimization targets. PAI is generally the stronger starting point when maximum load-bearing capacity, stiffness, high-temperature structural integrity, and wear resistance are the primary requirements. Its higher density and material cost can be justified when performance and service life are critical.
PEI offers a lower-density alternative with a strong balance of mechanical performance, impact resistance, thermal capability, chemical stability, and fabrication practicality. It is often the better value when the operating environment is demanding but does not require the highest PAI capability.
Before releasing a design, we recommend confirming the exact material grade, density, temperature limits, mechanical data, wear data, chemical compatibility, and machining requirements in the manufacturer’s material data sheet. For a custom CNC part, also review wall thickness, tolerances, threads, clamping, surface finish, and inspection requirements.
Our recommendation
Choose PAI for maximum strength and wear performance; choose PEI when you need high performance with lower density, broad capability, and a more balanced cost profile. If the decision affects a critical assembly, share the application conditions with us before finalizing the material.
Discuss your part
Need help selecting PAI or PEI for a machined component?
Send us your 2D drawing, 3D model, sample, quantity, tolerance, and application details. We can review the material choice and manufacturing approach for prototypes, low-volume production, and repeat custom plastic parts.